
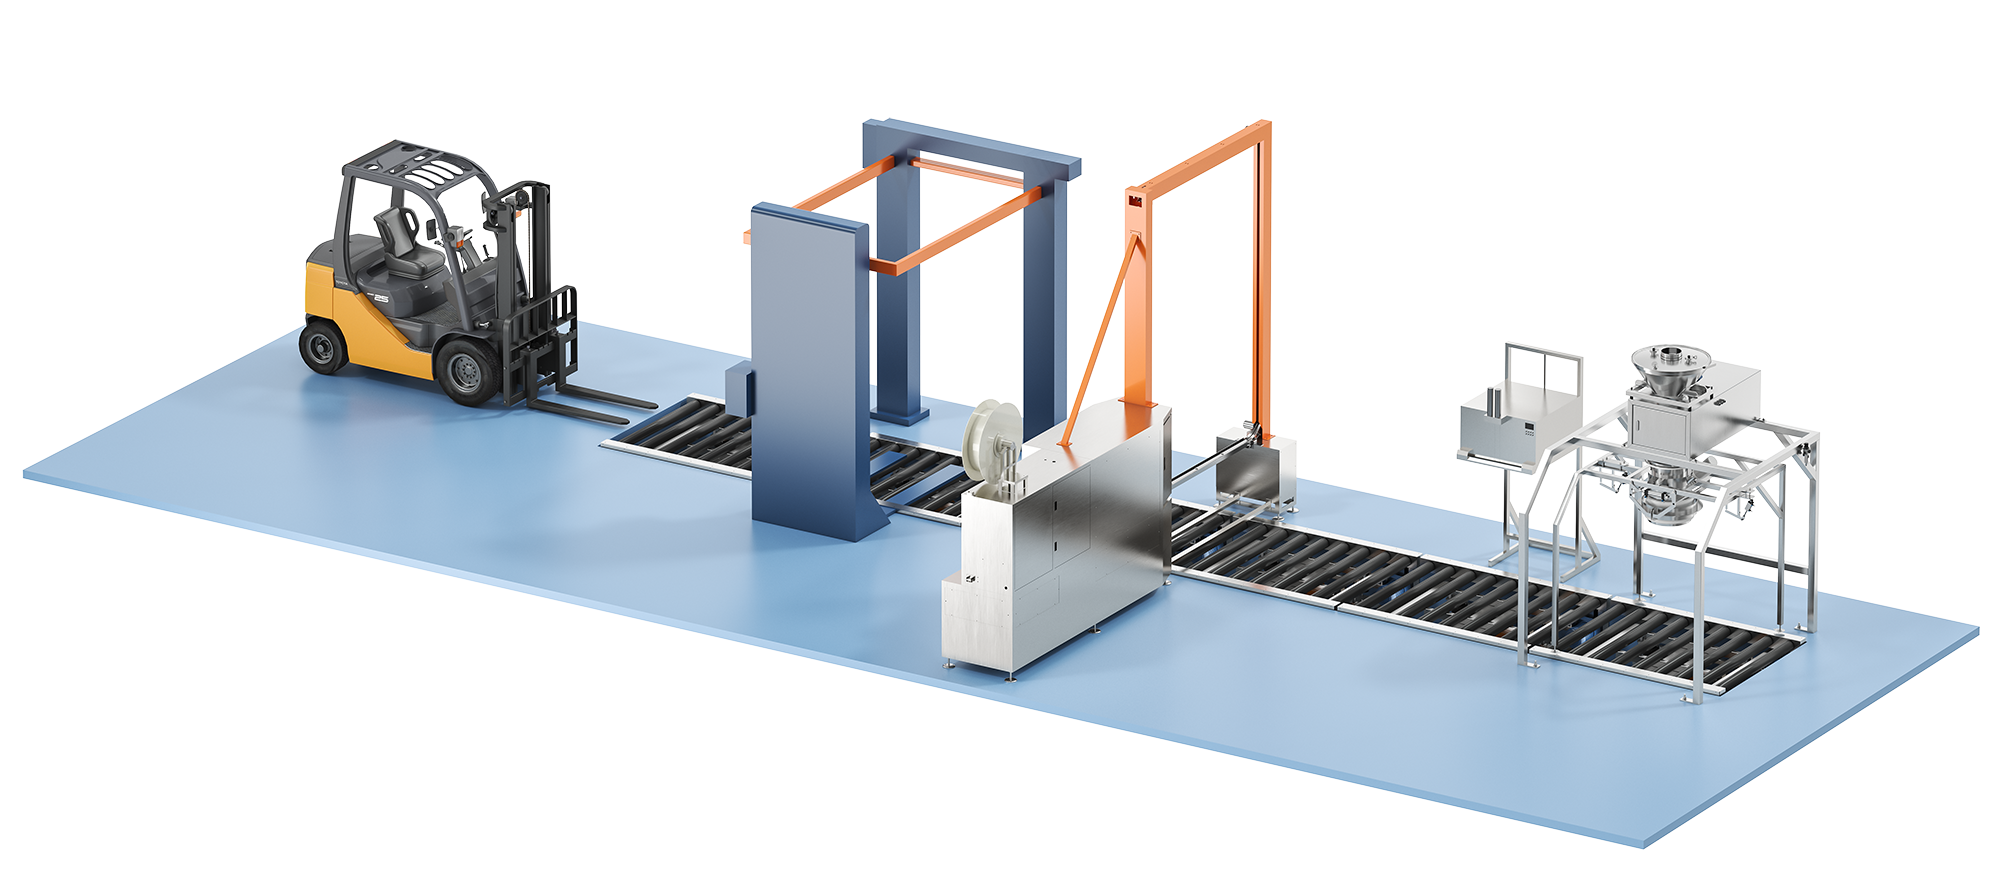
吨袋包装系统



Details:
This dustless feeding station is specially designed for dust-free unpacking and feeding of bagged materials. Adopting hygienic and ergonomic design, it complies with FDA/GMP industry certification requirements. Equipped with a sintered stainless steel mesh filter, it delivers high filtration precision and long service life, Its table-top structure facilitates convenient bag placement and operation, and it can be configured with an inline screener for expanded functionality. The system supports PLC-controlled automatic one-key start/stop operation, while integrated fan installation reduces on-site construction work and saves installation space. Available in multiple models, it offers a processing capacity of approximately 2000-3000 kg/h, making it widely applicable to powder feeding applications in industries including pharmaceuticals, food, chemicals, materials, and additives.
Technical Specification:
Core Advantages
Hygienic and ergonomic design complies with FDA and GMP certification requirements.
Sintered stainless steel mesh filter offers high filtration precision and long service life.
Table-top structure allows convenient bag placement and feeding operation.
Optional inline screener can be configured for integrated expanded functionality.
PLC automatic control with one-key start/stop enables easy operation.
Integrated fan installation reduces construction work and saves installation space.
Product Features
This dustless feeding station features hygienic, FDA/GMP-comliant construction, high-precision sintered stainless steel filters, a user-friendly table-top design, optional inline screening, PLC automatic control with one-touch operation, integrated fans for space savings, and multiple models offering capacities from ~2000 to ~3000 kg/h to meet diverse production needs.
Product Applications
Designed for dustless unpacking and feeding of bagged powder materials, this equipment is widely used in industries including pharmaceuticals, food processing, chemicals, advanced materials, and additive manufacturing to ensure clean, efficient, and contamination- free material handling.
Precautions
Install the unit on a stable, grounded surface, do not exceed its rated capacity, regularly clean and maintain filters and the integrated fan, disconnect power before servicing, comply with explosion-proof standards in hazardous environments, and follow all safety protocols during operation and maintenance to ensure safe, long-term use.
Pictures of factory:
Why Choose Us
1. Engineering depth
Layouts are checked against your P&ID and hazard study to align interfaces, venting, and access platforms with site standards.
2. Manufacturing traceability
Material certificates and weld maps can be bundled for FAT documentation, supporting audit-ready pharmaceutical projects.
3. Lifecycle support
Spare parts kits, on-site commissioning, and remote guidance shorten startup time and keep feeding performance stable.
FAQ
Q: How often does the sintered stainless steel filter need replacement?
A: The sintered filter is highly durable and typically lasts several years. Replacement is only needed when visible damage or a significant drop in suction performance occurs.
Q: Can the station handle sticky or moist powders without clogging?
A: For sticky or moist materials, an optional inline screener can be added to break agglomerates. Regular filter cleaning is also recommended for such applications.
Q: Is the integrated fan powerful enough for long conveying distances?
A: The integrated fan is designed for localized dust capture at the feeding point. For long-distance material transfer, an external vacuum blower should be added.


